Skip to content
HIGHLIGHTS
- STP operators use the AdiNexus Industrial IoT Gateway to collect and centralize process data from pumps, blowers, sensors, meters, PLCs, and other treatment equipment.
- The gateway connects flow meters, level sensors, pH sensors, turbidity sensors, dissolved oxygen instruments, energy meters, PLCs, and other STP field devices into a unified data collection environment.
- Multi-protocol connectivity enables integration between STP equipment, PLC systems, SCADA platforms, and cloud monitoring applications.
- Edge data processing supports real-time STP process data acquisition, local processing, event detection, and data logging—even during network interruptions.
- Secure remote connectivity allows operators to monitor flow, tank levels, water quality parameters, equipment status, energy data, and treatment process conditions from centralized locations.

The Challenge – STP Process Data Acquisition
Sewage treatment plants contain multiple treatment stages, equipment groups, instruments, and control systems that continuously generate operational data. When this information remains distributed across individual PLCs, controllers, meters, and field devices, obtaining a centralized view of the complete treatment process can become difficult.
- Distributed STP Equipment Data – Pumps, blowers, mixers, sensors, meters, and PLCs generate process data across different areas of the treatment plant.
- Multiple Data Sources – Different equipment and instruments may use different communication protocols and interfaces, making centralized data collection more challenging.
- Limited Process Visibility – Operators may need to access multiple control systems to view flow, level, water quality, equipment status, and other important process parameters.
- Manual Data Collection – Without automated data acquisition, process information may require manual recording or separate systems, reducing the availability of consistent historical data.
- Delayed Equipment & Process Events – Pump faults, blower issues, abnormal tank levels, communication failures, and process parameter changes can be difficult to identify without connected data.
- Connectivity Interruptions – Network interruptions can affect the availability of plant data when there is no local buffering or edge-level data handling.
Key Benefits for STP Process Data Acquisition
Operational Benefits
- Centralized collection of STP process and equipment data
- Real-time visibility of pumps, blowers, mixers, and field devices
- Continuous monitoring of flow, levels, and treatment parameters
- Improved visibility across different treatment stages
- Faster identification of abnormal equipment conditions
- Reduced dependence on manual process data collection
Financial Benefits
- Helps reduce operational downtime through better equipment visibility
- Supports monitoring of pump and blower operating conditions
- Helps identify energy consumption patterns
- Reduces manual data recording and monitoring effort
- Supports better maintenance planning using historical equipment data
Technical Benefits
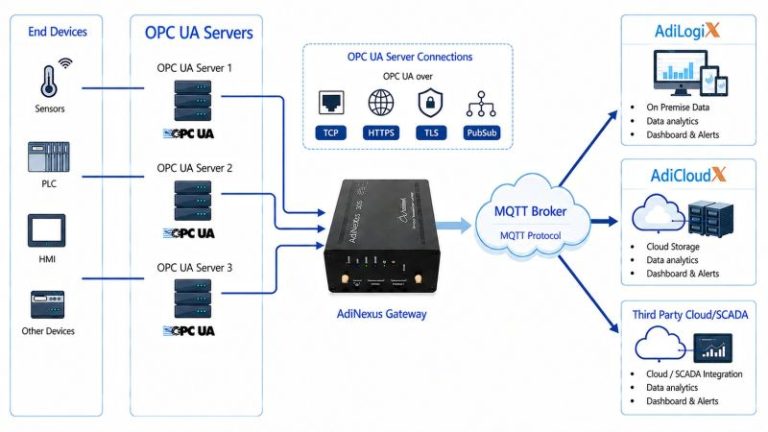
- Supports Modbus, OPC-UA, and MQTT connectivity
- Connects PLCs, sensors, meters, pumps, blowers, and other field devices
- Provides edge-level data acquisition and processing
- Supports local data logging and buffering
- Enables integration with SCADA and cloud monitoring platforms
- Provides secure communication between connected industrial devices and monitoring systems
Wastewater Treatment Benefits
- Centralized visibility of treatment process parameters
- Monitoring of inlet and outlet flow conditions
- Continuous visibility of tank and sump levels
- Monitoring of pH, turbidity, and dissolved oxygen data
- Better visibility into equipment and treatment process conditions
The Solution – STP Process Data Acquisition with AdiNexus
The AdiNexus Industrial IoT Gateway provides a connectivity and data acquisition layer between sewage treatment plant equipment and centralized monitoring platforms. It collects operational information from PLCs, sensors, meters, pumps, blowers, and other field devices and organizes the data for further monitoring and analysis.
By performing data acquisition and processing at the edge, AdiNexus helps maintain a continuous flow of STP process information. The collected data can then be transferred to SCADA, cloud, or other centralized monitoring applications for dashboards, historical analysis, and plant-level visibility.
Integrated Systems
AdiNexus connects with:
- STP PLCs and controllers
- Sewage and transfer pumps
- Aeration blowers
- Mixers and agitators
- Flow meters
- Level sensors
- pH sensors
- Turbidity sensors
- Dissolved oxygen instruments
- Energy and power meters
- Valves
- Supporting field devices
Supports Modbus, OPC-UA, and MQTT for connecting different industrial devices and monitoring platforms.
Real-Time Monitoring & Alerts
Operators can monitor:
- Pump operating status
- Blower operating status
- Inlet and outlet flow
- Tank and sump levels
- pH values
- Turbidity values
- Dissolved oxygen
- Pressure parameters
- Energy and power data
- Equipment alarms and faults
- Communication status
This provides centralized visibility into STP equipment operation and treatment process data.
Edge Data Collection
AdiNexus processes STP data close to the field equipment:
- Automatic STP data acquisition
- Local parameter monitoring
- Data processing at the edge
- Event and alarm detection
- On-gateway data logging
- Local data buffering during connectivity interruptions
Collected data can be synchronized with connected monitoring platforms after network connectivity is restored.
Equipment Fault & Process Event Monitoring
The gateway can make configured STP equipment and process conditions available to operators, including:
- Pump faults
- Blower faults
- Equipment status changes
- Abnormal tank levels
- Flow variations
- Water quality parameter changes
- Communication failures
- Configured operating thresholds
This helps operations and maintenance teams identify equipment and process conditions that may require inspection or maintenance.
Cloud & SCADA Integration
Collected STP data can be connected to:
- STP SCADA systems
- Cloud monitoring platforms
- Wastewater treatment dashboards
- Process analytics applications
- Central control room systems
- Plant performance monitoring platforms
This enables data from multiple STP sections to be accessed through a centralized monitoring environment.
Secure Data Communication
AdiNexus supports secure connectivity between STP equipment and monitoring platforms through:
- Encrypted data transmission
- Secure device communication
- Firewall protection
- Role-based access control
- VPN-ready connectivity
- Remote firmware updates